Semiconductor Equipment
Chamber parts, flanges, connector housings and test-fixture components. Vacuum-compatible finishes, demagnetized where required.
- AL6061 / A5052 / A5056
- 316L, ASTM A582
SEMICONDUCTOR · MACHINE TOOL · AUTOMATION
We're a trading and export company in Dalian, China. We don't run a factory: we match each part to a shop we've audited, hold the contract, inspect the result and ship it. 5-axis, turn-mill and precision grinding for semiconductor, machine-tool and automation OEMs.
PRIMARY FOCUS
Chamber components, flanges, feed-through housings and test plates — held on flatness and sealing faces, documented with CMM and material reports. The machine-tool and automation work we quote comes from the same group of shops.
WHAT WE SOURCE
The shops we work with run on semiconductor equipment parts, machine-tool components and automation hardware — the kind of work where a 5 µm error shows up downstream.
Chamber parts, flanges, connector housings and test-fixture components. Vacuum-compatible finishes, demagnetized where required.
Spindle housings, chuck bodies, guide-rail bases and bearing seats — ground and inspected for runout, not just dimension.
Reference pads, jig plates, jaws, connectors and brackets — often the parts that decide whether a line repeats within tolerance.
Pinion shafts, tie rods, stepped spindles and rotor shafts — turned, milled and ground in one setup where the geometry allows.
Frames, enclosures and large welded structures, machined after welding so the mounting faces stay flat.
Injection moulds, stamping dies and hardened inserts, including wire-EDM details and mirror-polished cavities.
CAPABILITIES
Turn-mill composite, 5-axis and precision grinding under one roof means fewer setups, fewer datum shifts, and tolerances that survive the last operation.
Milling and turning in one setup for coaxial features and tight runout.
Contoured faces, undercuts and gantry-sized frames.
Hardened parts, bearing seats, runout to 0.002 mm.
Sharp internal corners and hardened tool steel details.
| Processes | 5-axis, turn-mill, turning, grinding, EDM, sheet metal |
|---|---|
| General tolerance | ±0.005 mm (job-dependent) |
| Runout / roundness | 0.002 mm on ground features |
| Surface finish | Ra 0.4 µm |
| Materials | Al, stainless, carbon & alloy steel, cast iron, tool steel |
| Heat / surface treatment | Hardening, anodize, sandblast, polish, demagnetize |
| Inspection | CMM reports, first article, material certs |
| Prototype lead time | 5–10 working days |
| Production lead time | 2–4 weeks typical |
| MOQ | 1 pc |
MATERIALS
Mill certificates supplied with every batch. Exotic grades sourced on request with full traceability.
WHERE IT GOES
Our parts end up inside semiconductor tools, machine tools, inspection systems and automation lines — usually as the component that has to be right the first time, because rework means a stopped line.
| Semiconductor | Chamber parts, flanges, feed-throughs |
|---|---|
| Machine tools | Spindle housings, chuck bodies, rail bases |
| Automation | Reference pads, jaws, tie rods, brackets |
| Inspection | Fixture plates, precision mounting bases |
| Mould & die | Inserts, cores, ejector components |
WORK
Real components, photographed after final inspection — fixture plates, hardened rails, turned families and anodized housings.
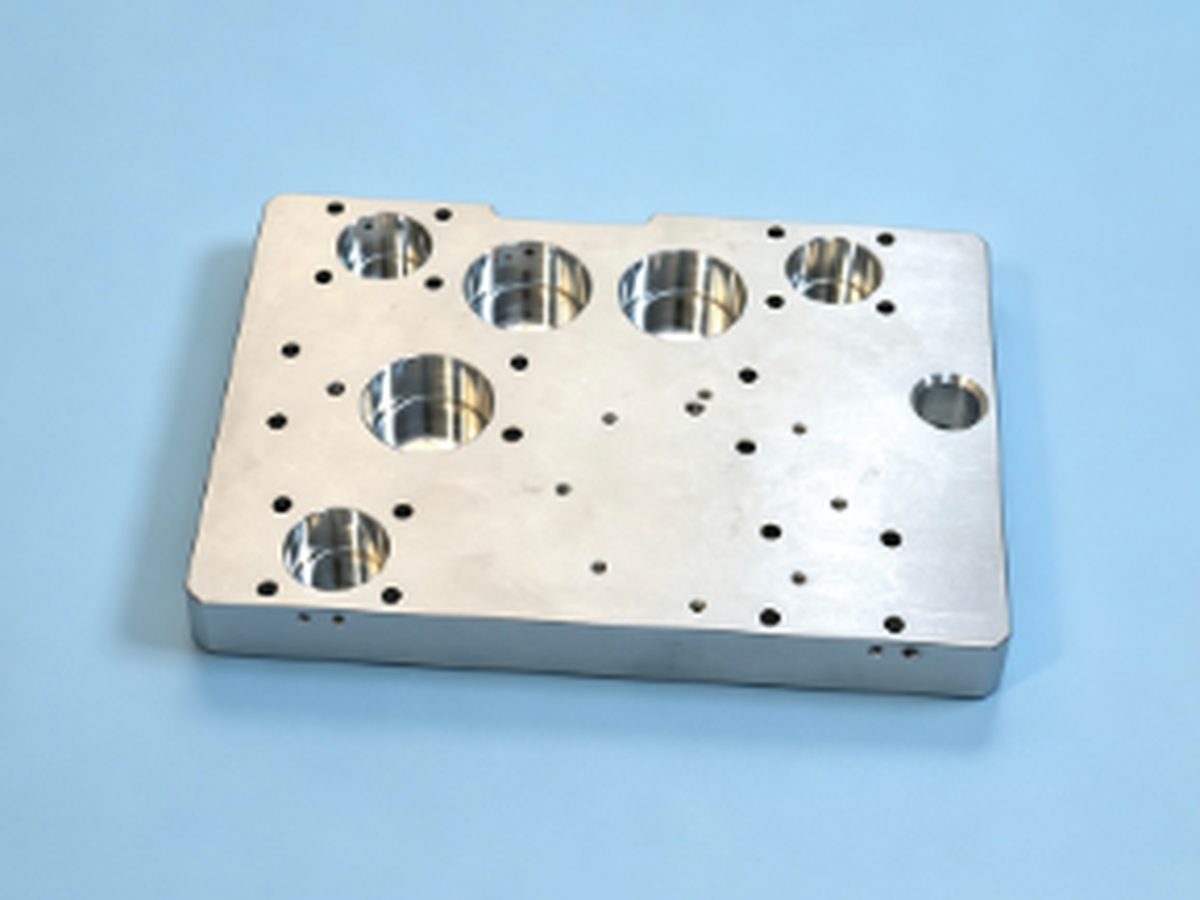 Fixture plate · AL 6061
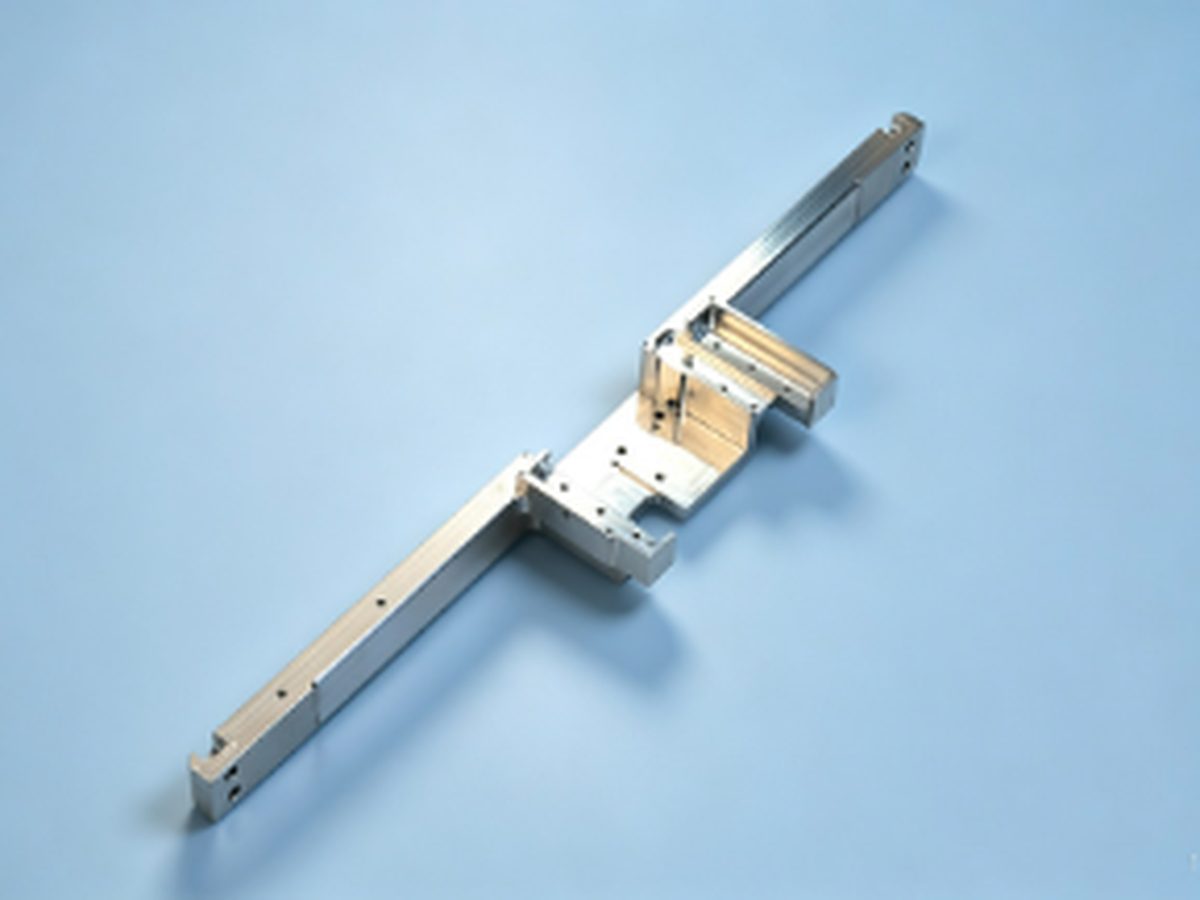 Bracket & shaft · turn-mill
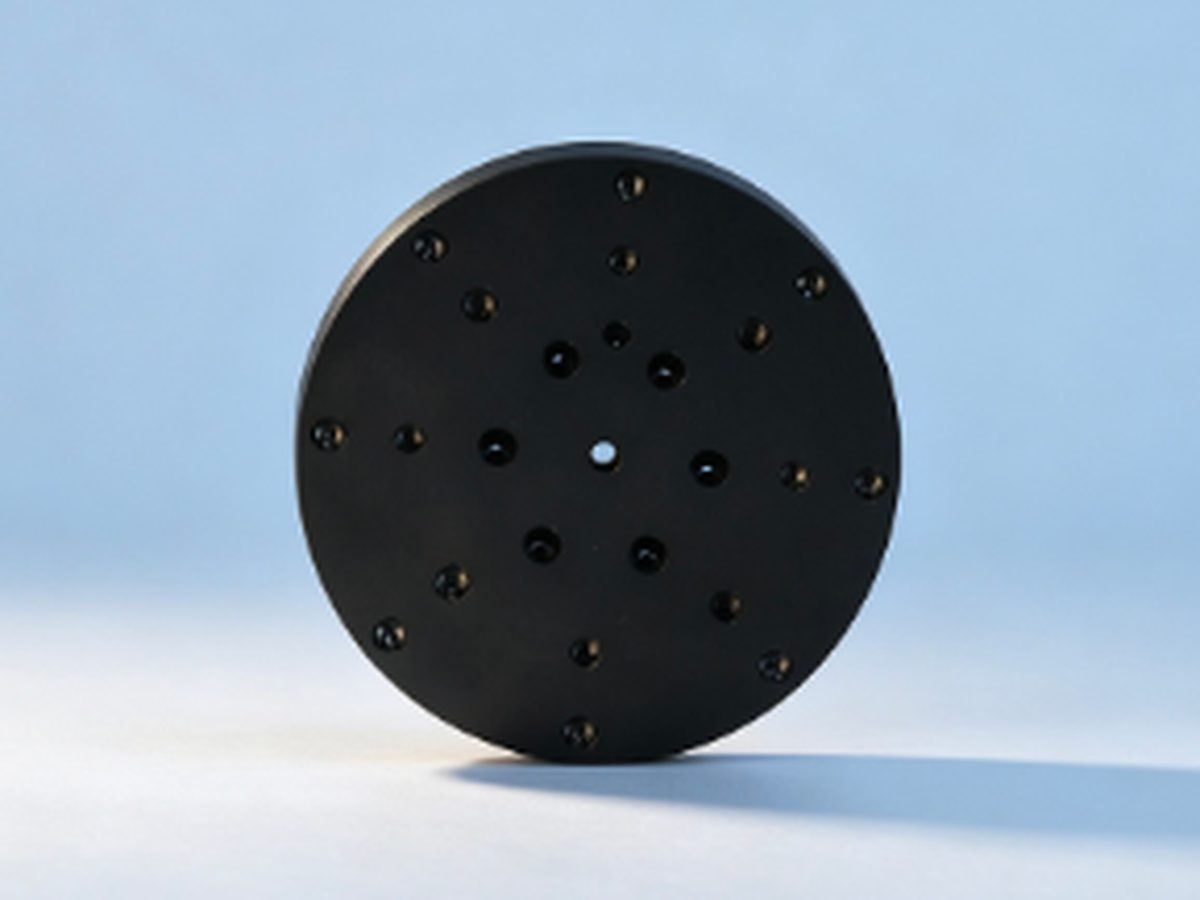 Anodized platen
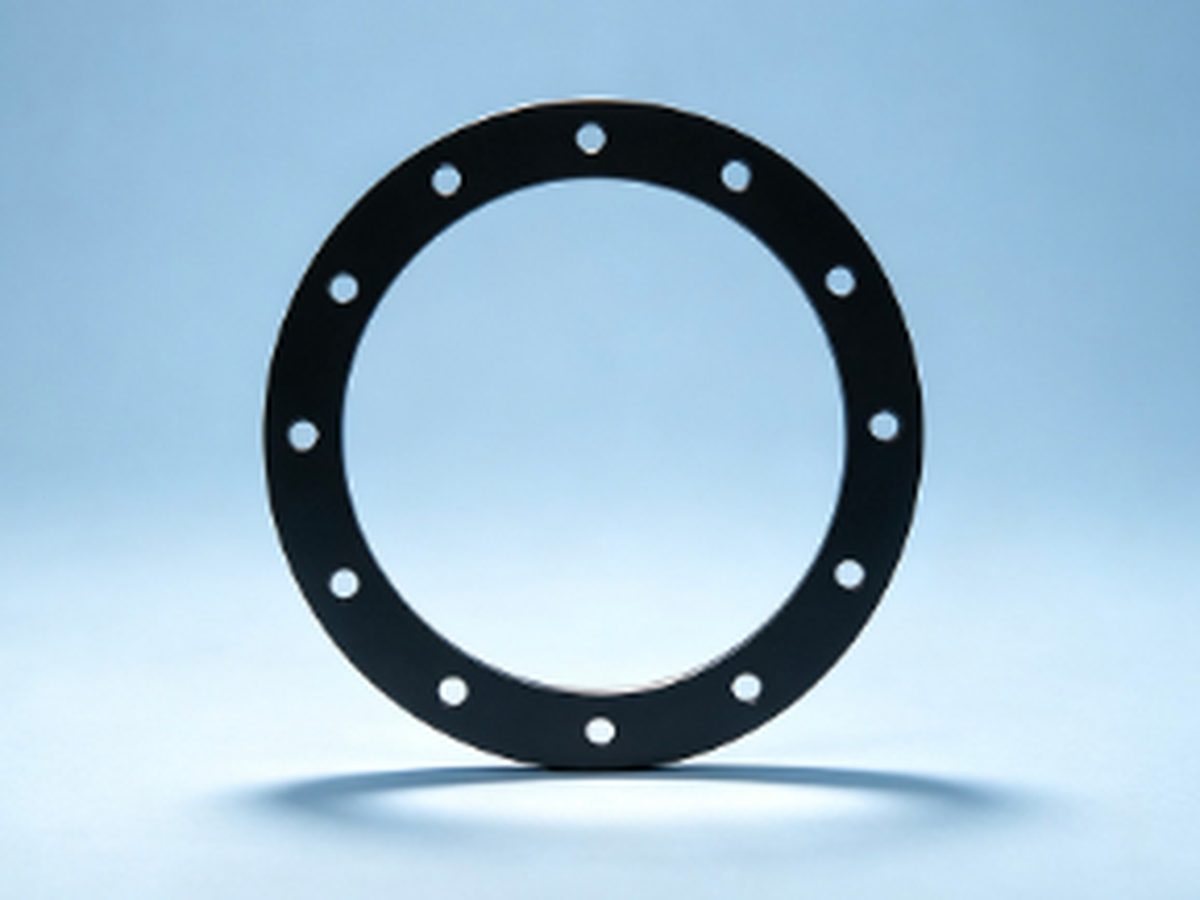 Ring flange · anodized
 Linear rail base · ground
 Turned parts · 316L / 42CrMo
 Star bracket · 5-axis
 Rail base · SKD11
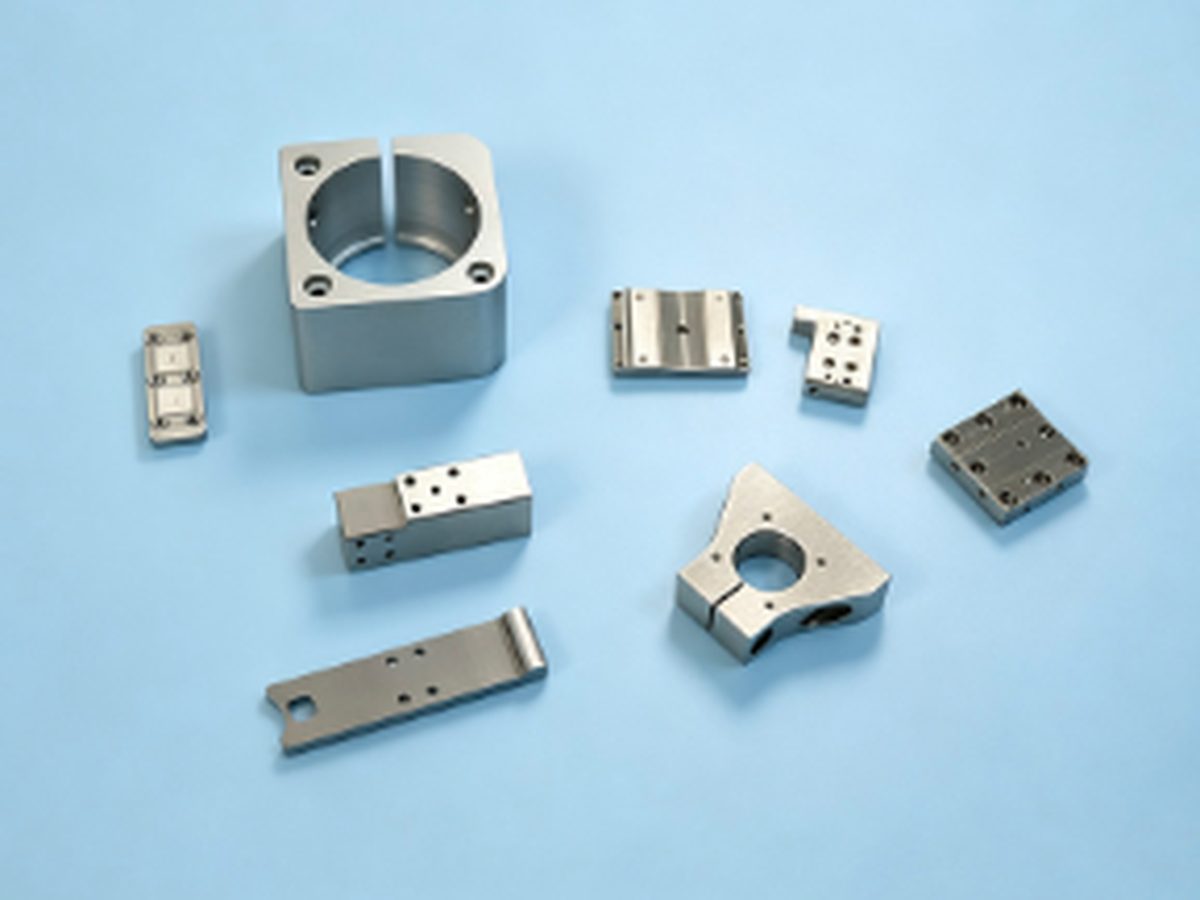 Precision blocks · SS400
INSIDE THE SHOP
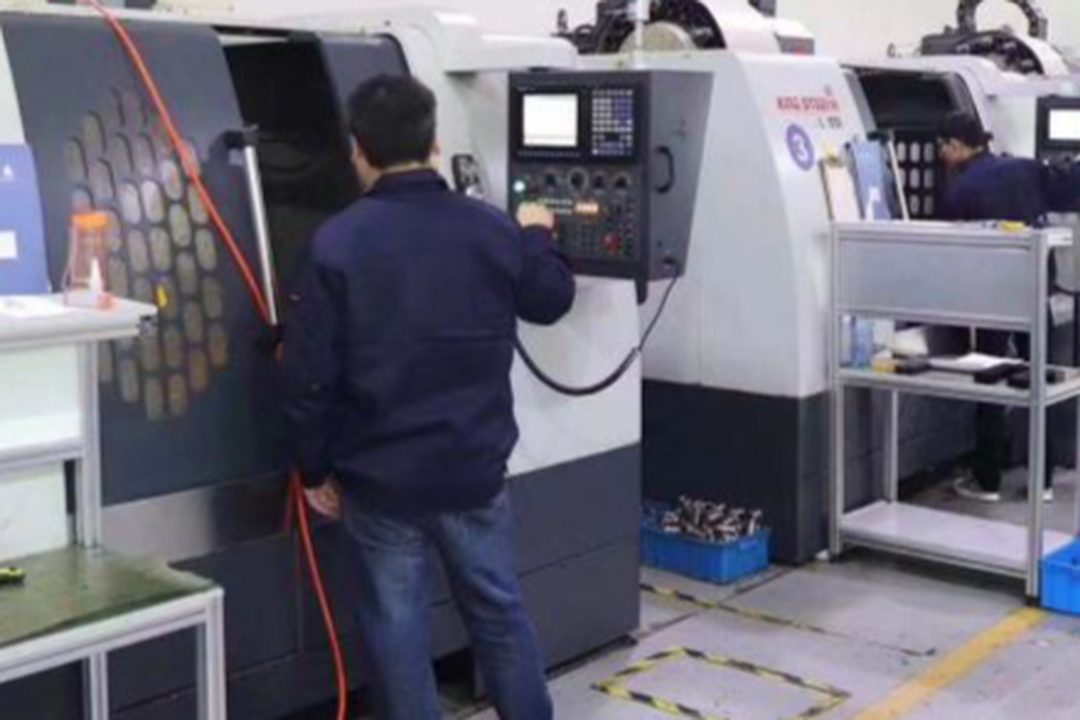
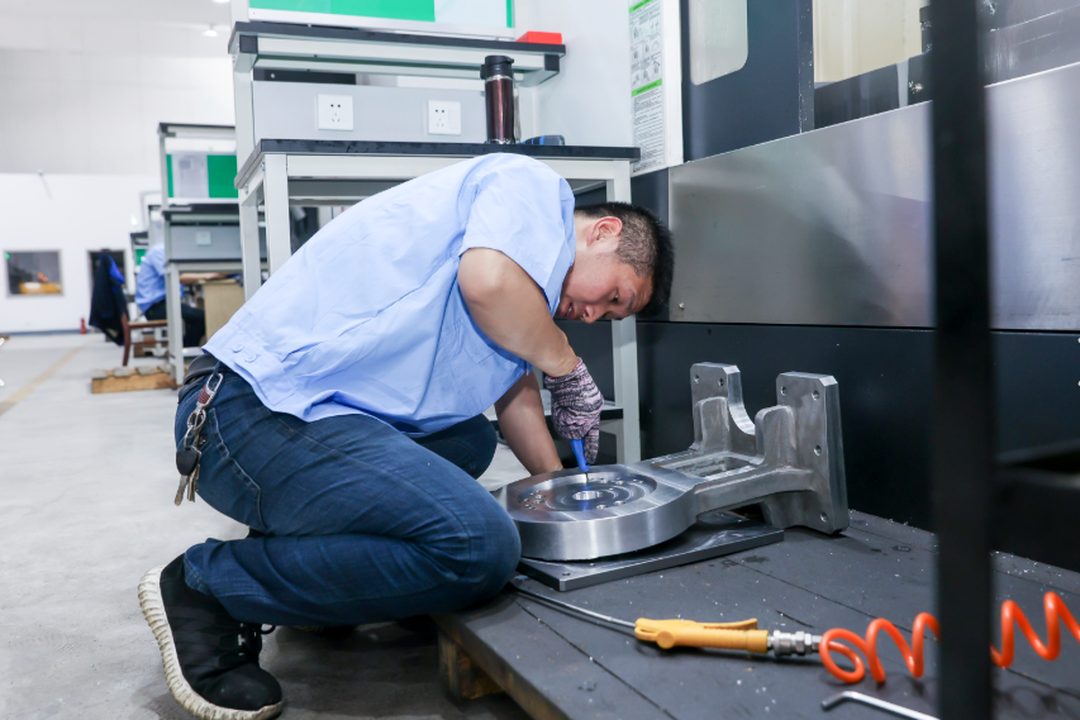
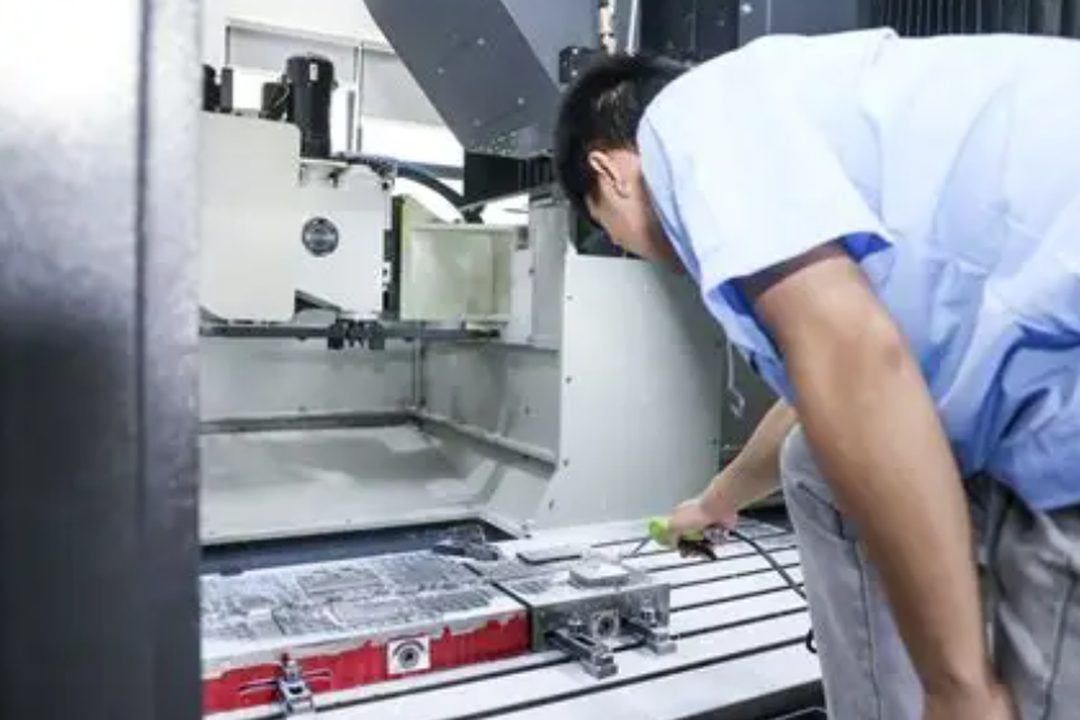
Turning cells, machining centres and fitting benches — photographed on a normal working day at one of our partner workshops in Dalian, China. The shop isn't ours; the accountability is.
CASE STUDIES
A seal that wouldn't hold, flatness that moved after coating, and a part with no drawing at all.
A Ø260 sealing face that has to stay flat through passivation — distortion removed before the finish cut.
380 holes at ±0.01 mm on a 320 mm plate, checked after black anodizing.
A worn sample becomes a model, a tooling plan and a fit-checked replacement.
QUALITY
Every batch leaves with a dimensional report. First-article, PPAP and material certificates are available on request. Certificates belong to the partner shops that make the parts, not to us — we send the certificate and its scope before you place an order, so you can check it against your own requirements.
FAQ
No — and we say so up front. We're a trading company in Dalian: we don't own machines or employ machinists. We qualify the shop, place the order, hold the inspection record and carry the risk. The part is made in a factory; the commitment is ours.
Yes. We arrange video walkthroughs and, for larger programs, on-site visits — under NDA if you prefer. The shop is not named publicly, but nothing is hidden from you once we're working together.
Parts where geometry, hardness and finish interact: spindle housings, chuck bodies, semiconductor chamber parts, hardened reference pads and shafts. If your part needs three setups and a grinding operation, we're in our element.
Yes — ours or yours, within one business day. Drawings stay on an access-controlled server and are never shared outside the shop.
30% deposit / 70% before shipment by T/T for most orders. L/C at sight for larger programs. Net terms can be discussed once a trading history is established.
Yes, to most destinations — we handle freight, duties and last-mile delivery. EXW, FOB and DAP are also available.
We issue a written NCR within 5 working days, then rework, replace or refund. The inspection report that ships with the batch makes it easy to check on arrival.
REQUEST A QUOTE
Tell us what you need and we'll reply within one business day with price, lead time, the process route we'd use and any DFM suggestions — no obligation.
Unit 43, Tian'an International Business Center, 88 Zhongshan Road, Zhongshan District, Dalian, Liaoning, China
Mon–Sat, 08:30–18:00 (GMT+8)