Chamber & vacuum components
Chamber bodies, lids, flanges and port plates. Ground sealing faces, controlled edge break, no tool marks on the vacuum side.
SEMICONDUCTOR EQUIPMENT · 5-AXIS · GRINDING
Chamber components, flanges, feed-through housings and test-fixture plates in aluminium and stainless. 5-axis machined, ground where flatness matters, and shipped with dimensional and material reports.
WHAT WE SOURCE
Most of this work is one-off or low volume, revised twice before release, and judged on flatness, hole position and surface condition rather than cycle time.
Chamber bodies, lids, flanges and port plates. Ground sealing faces, controlled edge break, no tool marks on the vacuum side.
Insulator housings, pin carriers and mounting bosses with tight position tolerance across multiple faces.
Probe cards, socket plates and alignment plates with dense hole patterns and flatness held across the full plate.
Sensor mounts, cable brackets and gantry parts — usually 5-axis, often anodized black.
Plates and rings machined from aluminium or engineering plastics, deburred and cleaned before bagging.
Reverse-engineered from a sample or drawing when the OEM lead time is measured in months.
MATERIALS & FINISHES
Semiconductor work rarely fails on dimensions alone. It fails on porosity, edge burrs, trapped moisture or a coating that flakes in vacuum. We pick the alloy for the chamber, not for the price list.
| AL 6061-T6 | Chamber bodies, plates · clear or black anodize |
|---|---|
| A5052 / A5056 | Housings, brackets · hard anodize, sandblast |
| SS 316L | Vacuum-side fittings · passivation, electropolish option |
| ASTM A582 | Turned details · passivation |
| PEEK / POM | Insulators, guides · machined, annealed on request |
TOLERANCES & FINISH
A part can be within tolerance and still leak. We control flatness, surface finish and edge condition on the sealing faces, and report them separately.
Angled ports, pockets and bosses without re-datuming.
Flatness and Ra verified, not assumed.
For parts that see charged beams or sensitive sensors.
| Materials | AL 6061, A5052, A5056, SS 316L, ASTM A582 |
|---|---|
| General tolerance | ±0.005 mm |
| Flatness | 0.01 mm typical on plates |
| Surface finish | Ra 0.4 µm ground; Ra 1.6 µm milled |
| Edge condition | Controlled deburr, no sharp edges on vacuum side |
| Finishes | Anodize (clear/black/hard), sandblast, polish, demagnetize |
| Cleaning | Degreased, bagged, handled with gloves |
| Documentation | CMM report, material cert by heat number |
| Typical lead time | 5–10 working days for samples |
FROM DRAWING TO DOCK
DFM notes within one business day: datums, features that need grinding, finishes that won't survive.
Alloy and stock size fixed, mill cert ordered, process route agreed before any cutting.
5-axis or turn-mill first, then grinding on the faces that seal or locate.
CMM report, flatness and finish checks, material cert matched to the batch.
Degreased, handled with gloves, bagged individually, DDP or DAP to your dock.
WORK
 Anodized platen
 Ring flange
 Fixture plate
 5-axis bracket
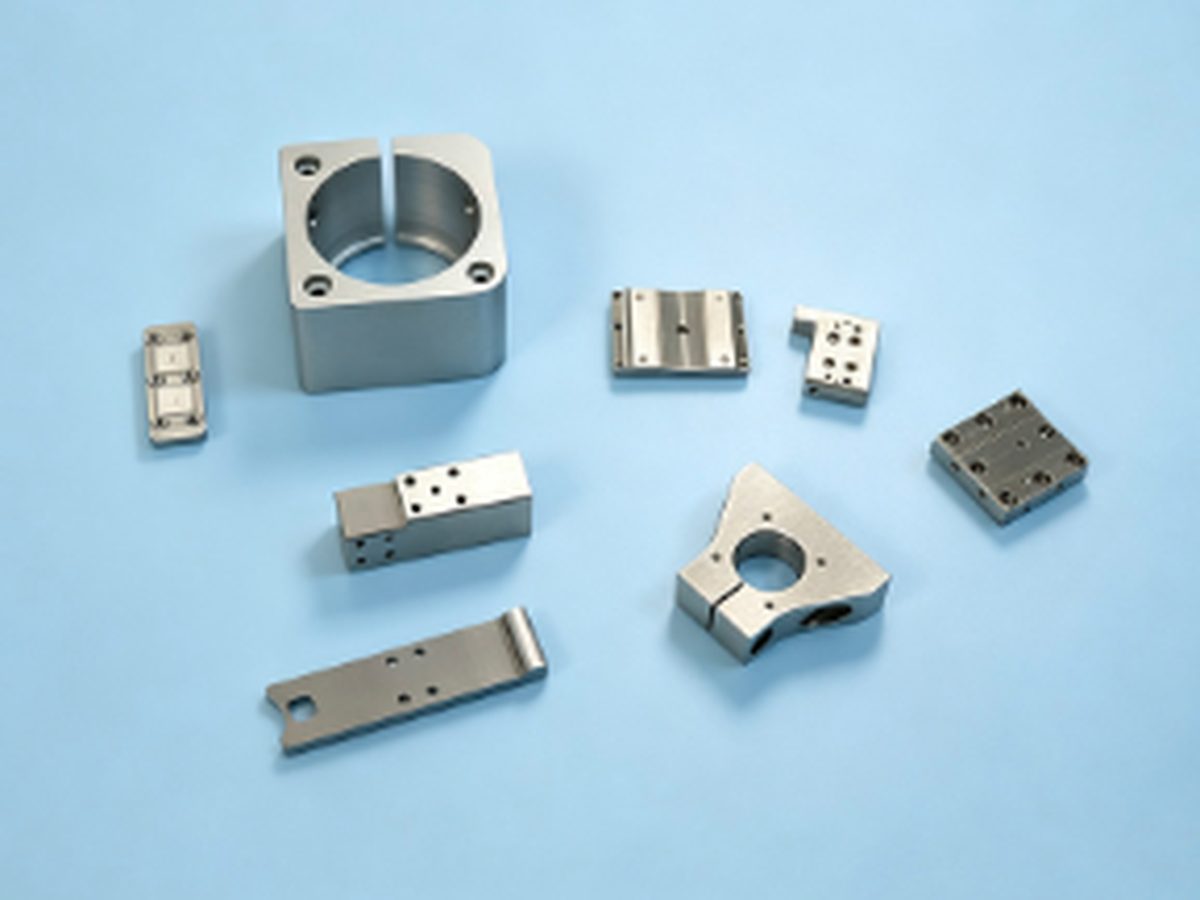 Small details
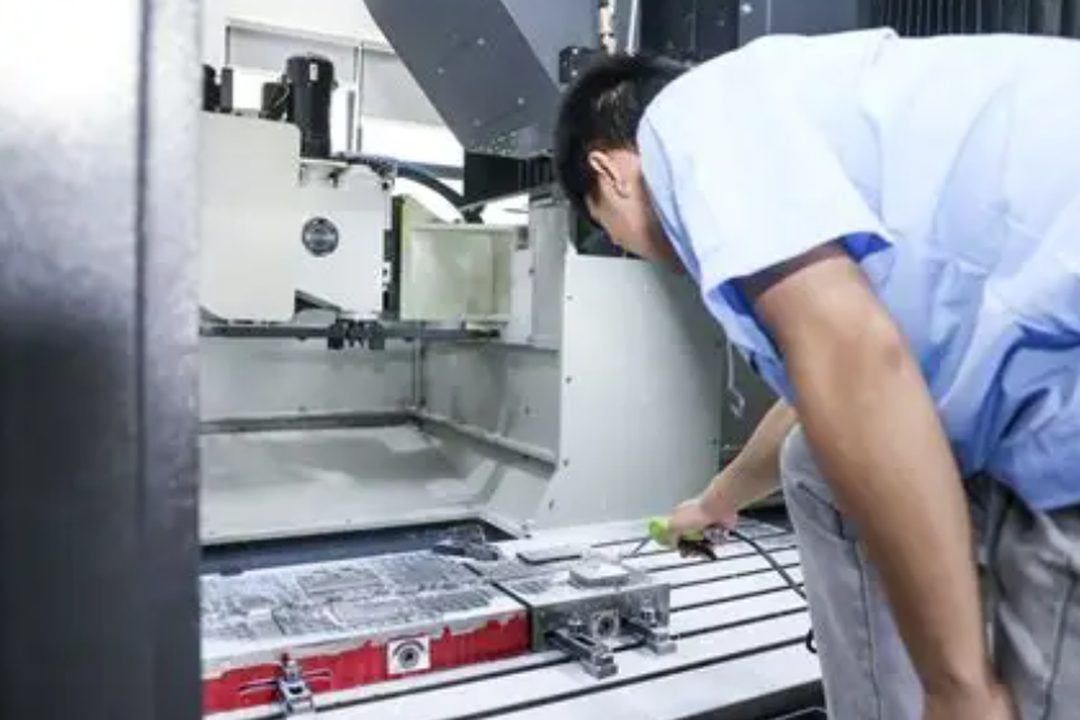 Set-up on the table
FAQ
Yes, from solid stock — no welds on the vacuum boundary unless you specify them. We can hold flatness and finish on sealing faces and supply the measurement report.
Yes. Clear, black and hard anodize with masking on threads, bores and electrical contact areas. Colour is matched to your sample or RAL code.
No, and we won't pretend otherwise. Parts are degreased, bagged and handled with gloves; if you need a specific cleaning protocol or particle count, send the spec and we'll say honestly whether we can meet it.
Five to ten working days for most single parts, including material purchase. Complex multi-setup parts take longer; we'll tell you before you order.
We have parts machined and inspected to the drawing and the standard you cite — dimensions, surface finish, edge condition and material. We don't issue SEMI compliance certificates ourselves; if you need third-party certification, we'll arrange the inspection body and quote it separately.
New revision, new part number, fresh first-article check. We won't quietly update a running batch — and if a change makes a feature ungrindable, you'll hear it before the chips fly.
No obligation, and we'll flag anything in the drawing that will cost you money later.