Reference pads & datum blocks
Hardened and ground pads, flat and parallel, used as the zero for everything else on the fixture.
AUTOMATION · JIGS · ROBOTICS
Datum blocks, jig plates, jaws, tie rods and brackets — the small, unglamorous parts that decide whether a line repeats. Cut from SS400, S45C, 16MnCr5 and SCM435, hardened and ground where it matters.
WHAT WE SOURCE
Fixture work is unforgiving: one part is easy, the tenth identical part is the job. We control datum faces, hole position and surface hardness together.
Hardened and ground pads, flat and parallel, used as the zero for everything else on the fixture.
Dense hole patterns, bored pockets and dowel locations, flatness held across the plate.
16MnCr5 jaws, case hardened where you need wear resistance, machined to your grip profile.
Turned rods with threaded ends and flats, straightness and thread runout checked.
Small 5-axis parts with angled faces, usually anodized or blacked to avoid reflections.
Guide blocks, stops and mounting plates, often paired with our linear rail bases.
TOLERANCES & PROCESS
We have the datum machined first, then everything else from it — and we measure position after hardening, because hardness and flatness fight each other.
Case or through hardening, then finish grinding to hold flatness.
Fixtures and programs kept, so the 50th part matches the first.
Laser or engraved part numbers for traceability at the line.
| Materials | SS400, S45C, 16MnCr5, SCM435, AL 6061 |
|---|---|
| General tolerance | ±0.005 mm |
| Flatness / parallelism | 0.01 mm typical |
| Hardness | Case hardened or through hardened on request |
| Surface finish | Ra 0.4 µm ground; Ra 1.6 µm milled |
| Finishes | Anodize, black oxide, sandblast |
| Inspection | CMM report, hardness check |
| Typical batch | 1 – 500 pcs |
| Typical lead time | 5–10 working days |
WORK
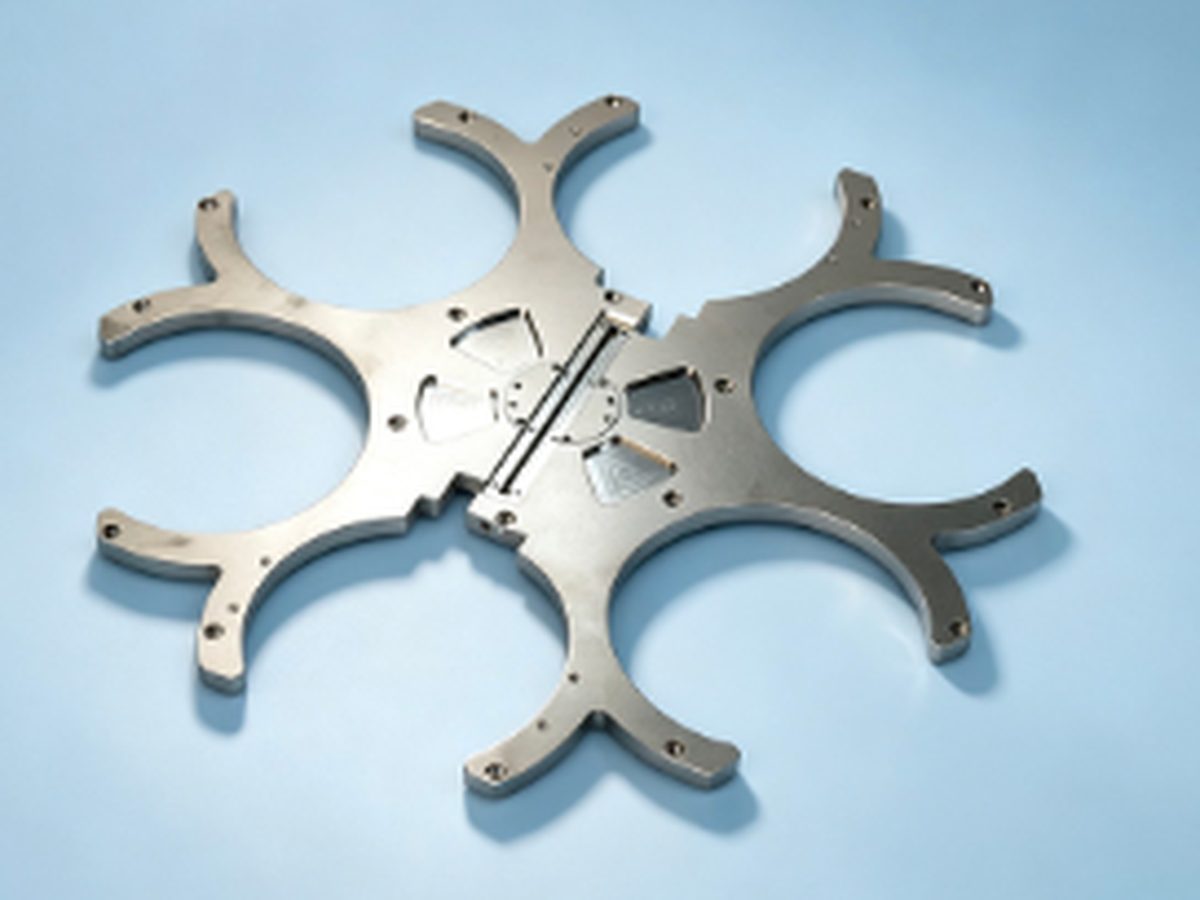 Star bracket · 5-axis
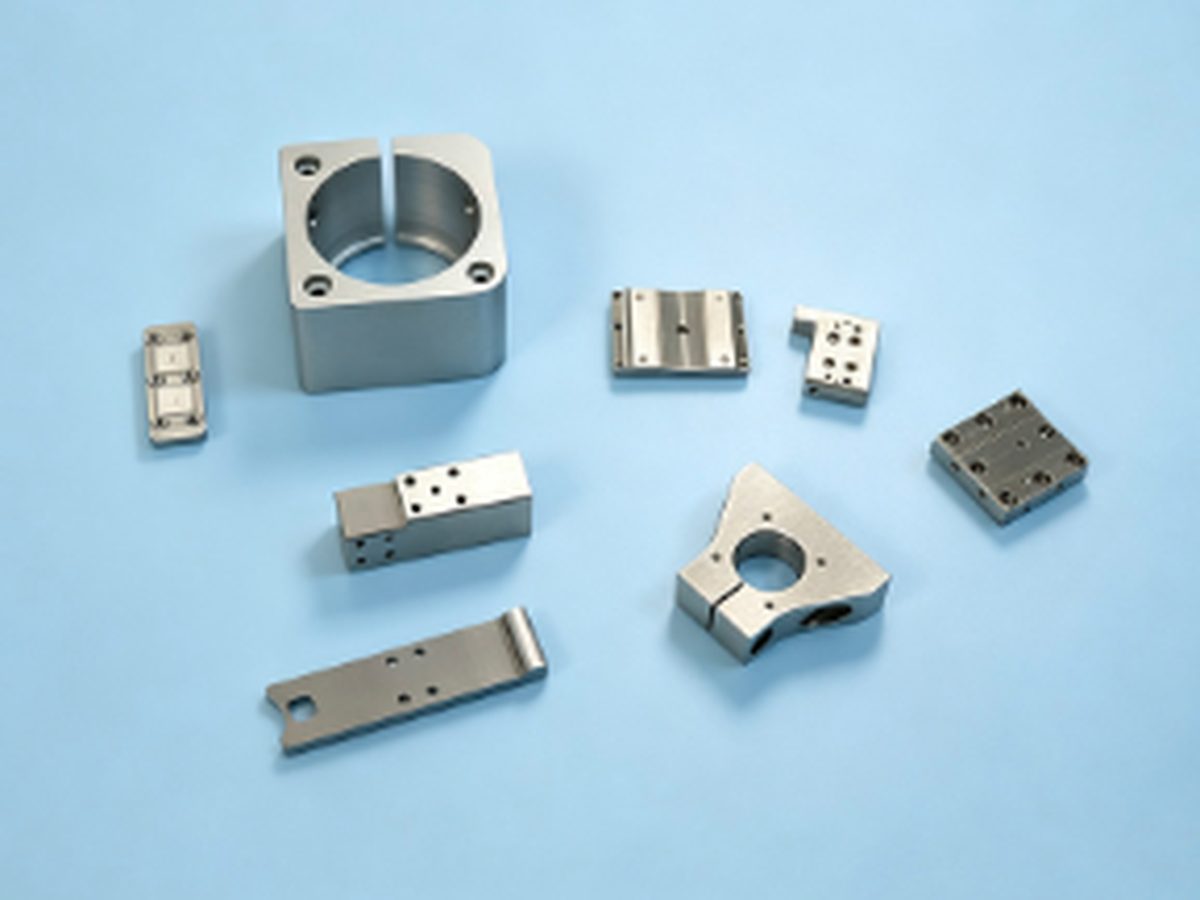 Fixture details
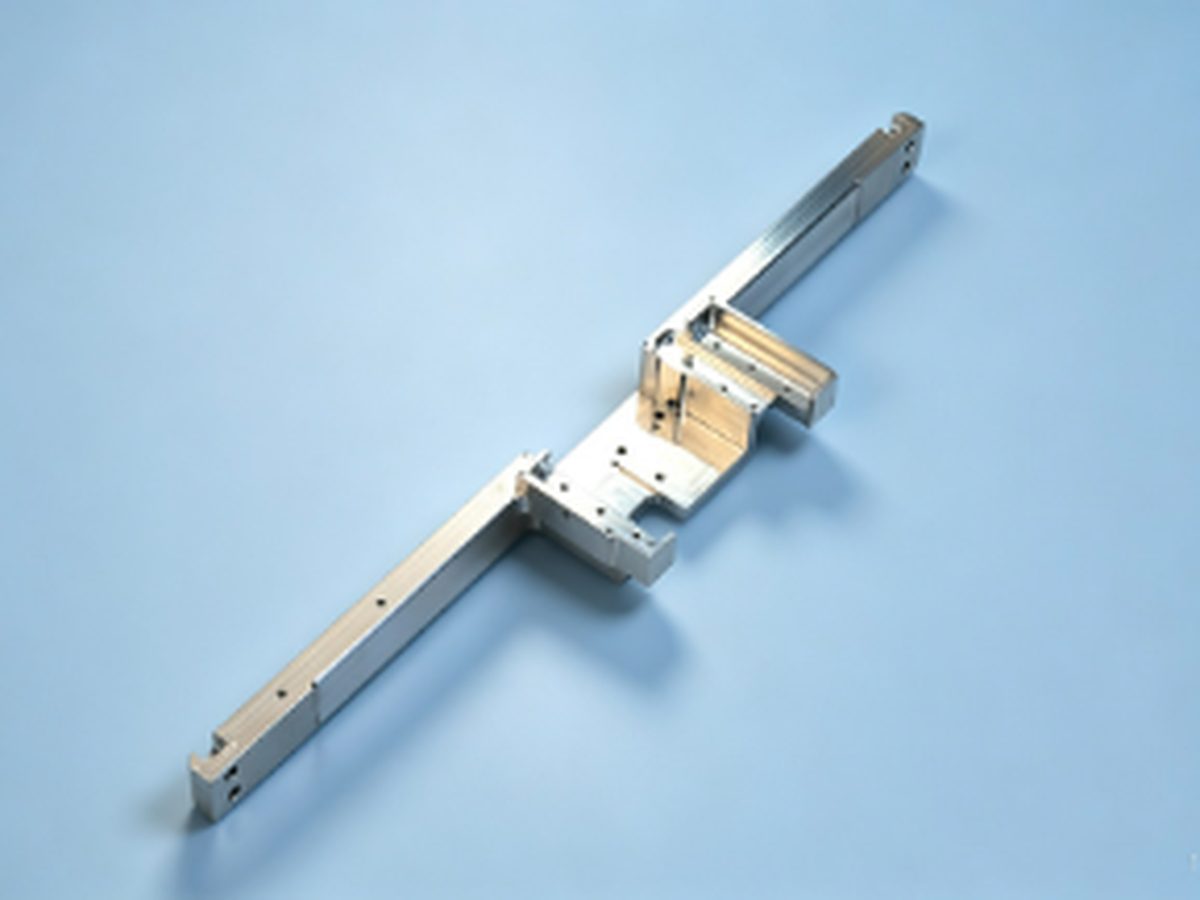 Bracket & shaft
FAQ
Yes, if the job stays in the same shop with the same fixtures — which is why we keep the program and fixture for repeat orders. We also report the first and last part of each batch.
Laser marking or light engraving, either on a machined face or a dedicated pad. Send the text, font size and position, and tell us if the surface is functional.
Every revision gets a new part number and a fresh first-article check. We won't silently update a running batch — if the rev changes, you'll see it in the quote.
We have fixture plates and details machined to your design. We don't design fixtures from scratch — that stays with your process engineer, which is where it belongs.
Small batches welcome — one piece is fine, and we'll tell you if hardening will move your datum.